Tough. Precise. Efficient.
Metal
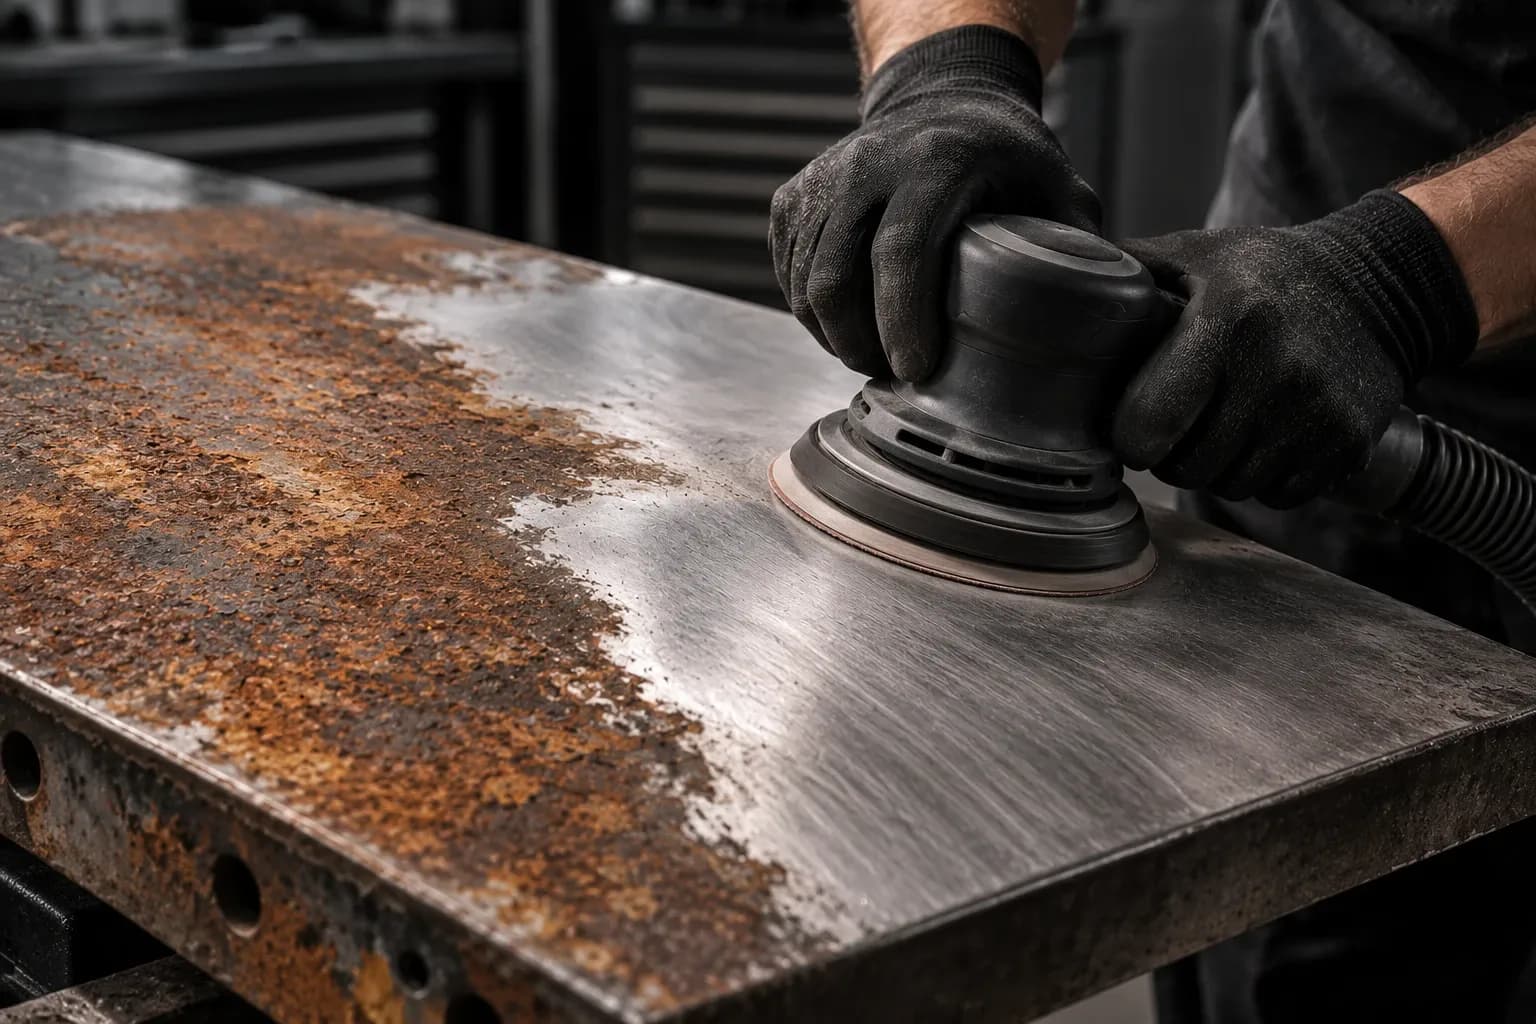
Remove rust, smooth welds, key surfaces or take off material precisely. For metalworkers, fabricators and workshops.
4 work stepsGrit P60 to P400With rust or scale from P40
The film
Sanding for metal
Remove rust with P40 to P80, blend with P80 to P240.
How to go about it
3 stages from coarse to fine – and where you start depending on the condition of the surface.
From raw to finished
Stage 1: Remove rust
P40 – P80
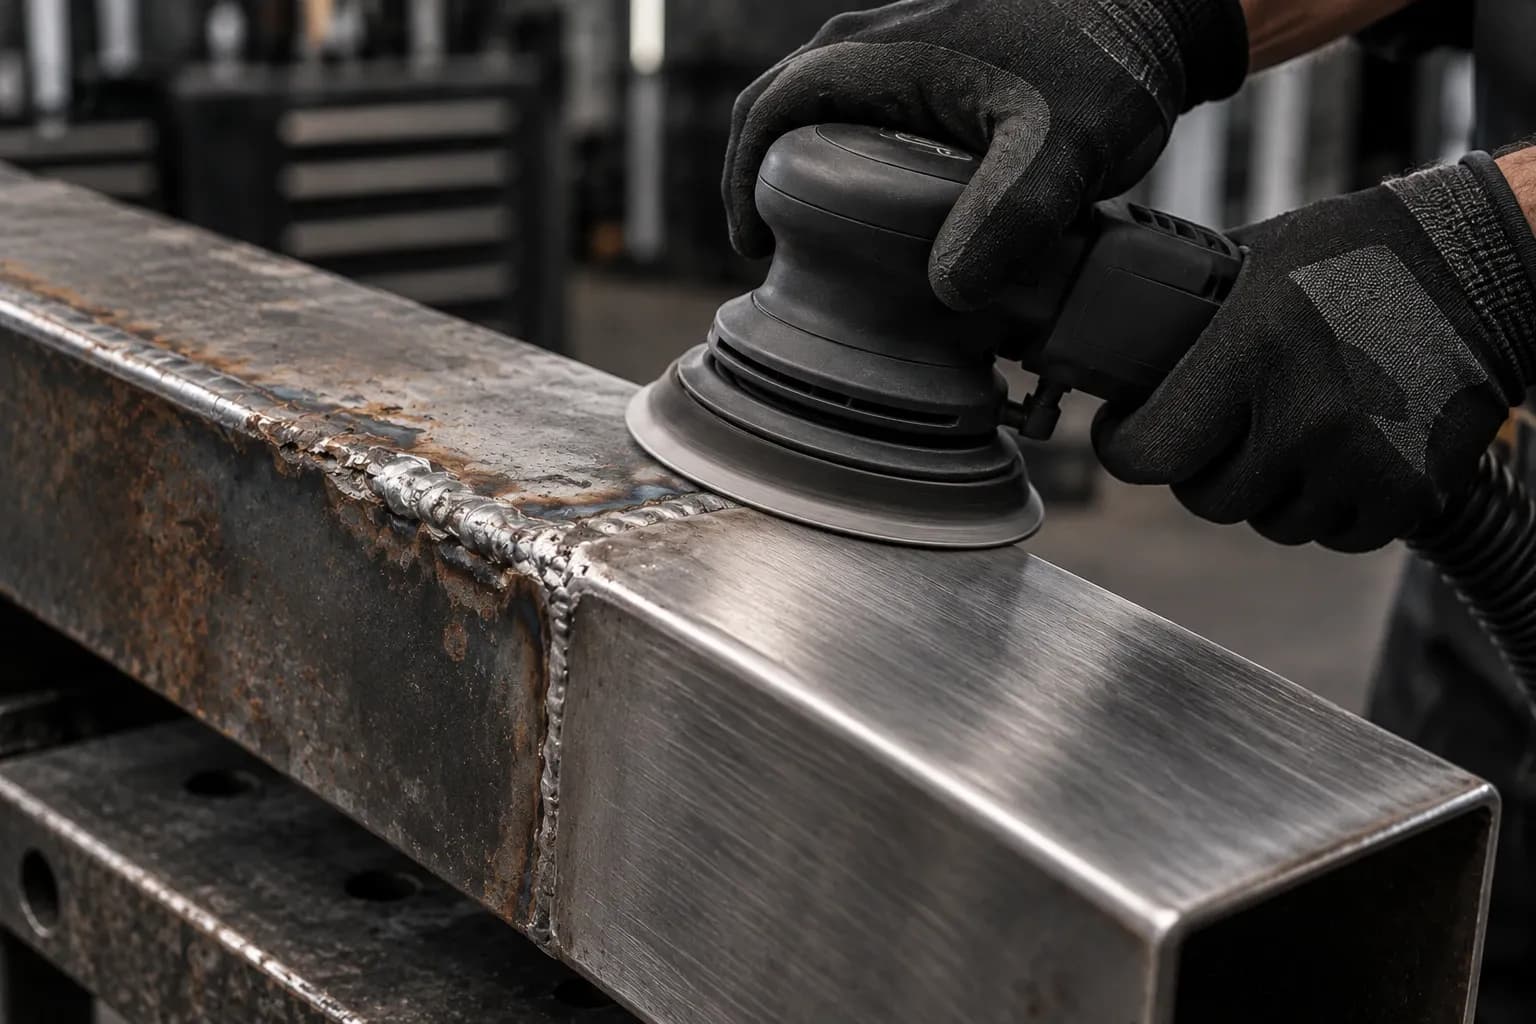
Stage 2: Dress & key
P80 – P240
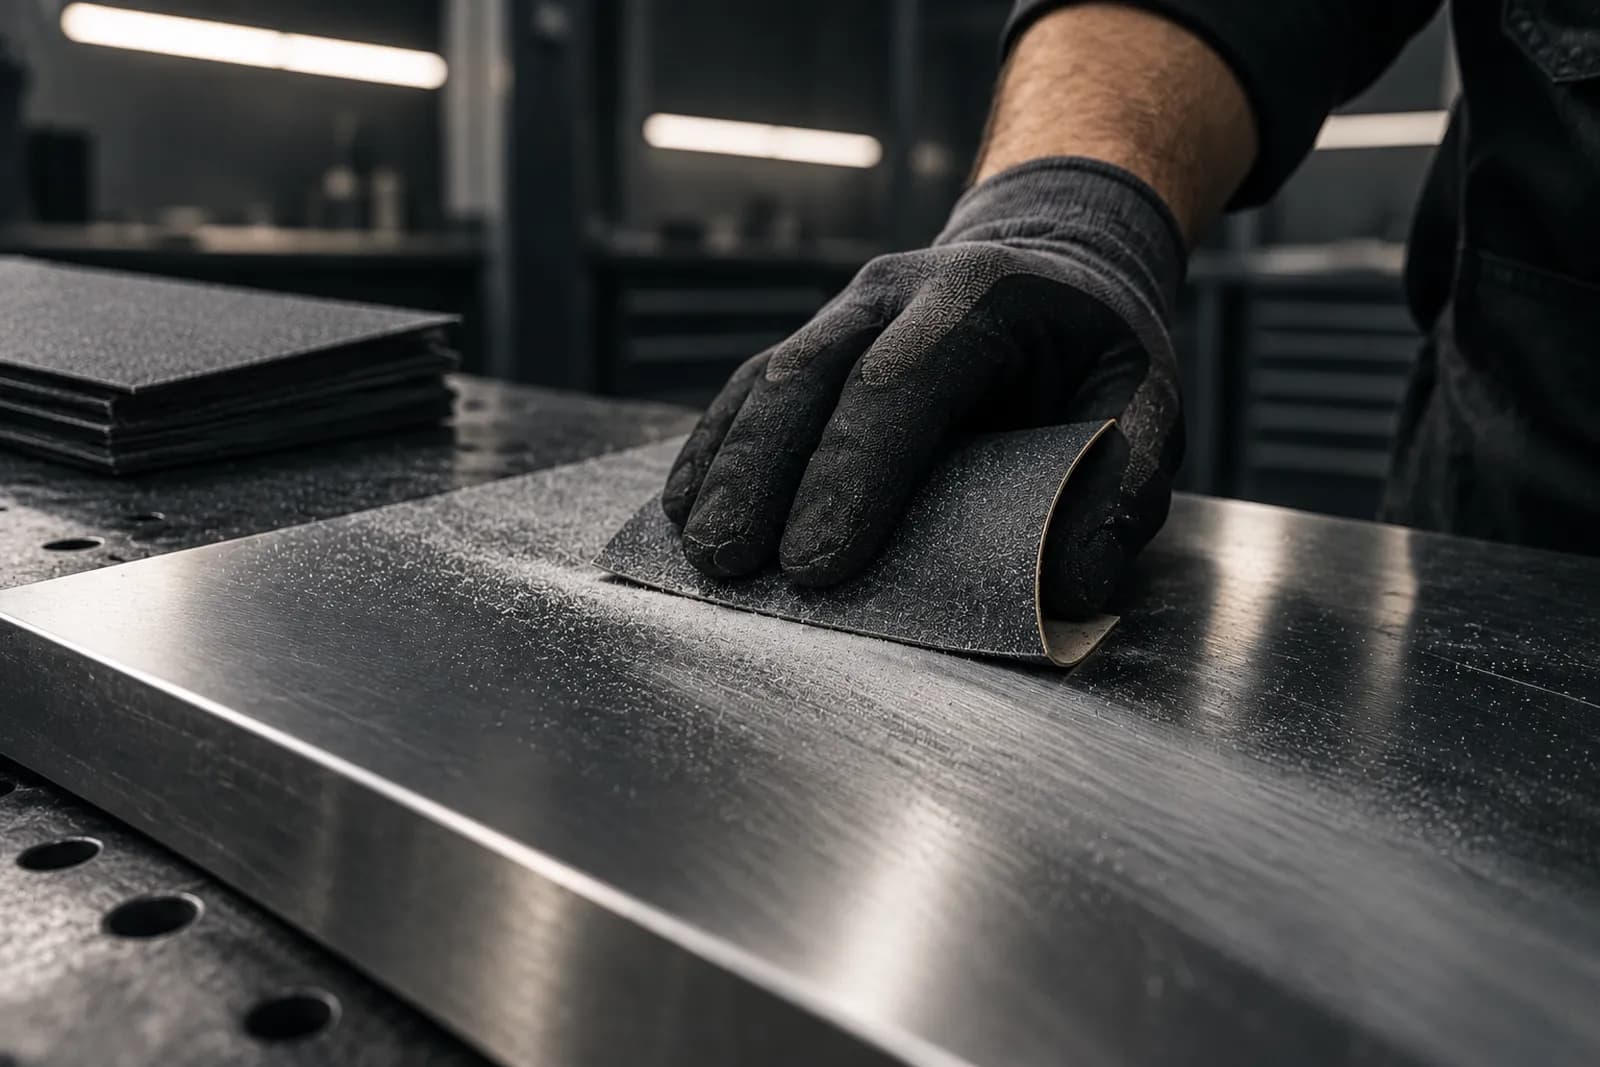
Stage 3: Fine sanding / finish
P240 – P400
Where do I start?
The starting grit depends on the condition of the surface – not everyone starts at step 1.
| Initial condition | Starting grit | Start |
|---|---|---|
| Heavy rust or mill scaleTackle thick patches with a flap disc first. | P40 | from step 1 ↓ |
| Flash rust | P80 | from step 1 ↓ |
| Fresh weldPre-grind thick welds with an angle grinder first. | P80 | from step 2 ↓ |
| Bare sheet metal, to be painted | P120 | from step 3 ↓ |
| Sound finish, just recoatingJust key it until everything is matt. | P180 | from step 3 ↓ |
| Scratched stainless steel, staying bareDedicated discs – steel particles rust on stainless steel later. | P240 | from step 4 ↓ |
Work steps
4 steps in working order – from coarse to fine. For each step, the grits and the matching product.
- 1
Remove rustOnly with rust or scale
Take rust, mill scale and old paint down to bare metal – heavy rust with P40 to P60, flash rust with P80.
Move on when: Bare metal everywhere, even in pits and pores – not a single brown spot left.
Tip: First go coarse down to bare material, then one grade finer over the whole surface – otherwise the P40 scratches show through primer, paint or oil. In the system: Remove old paint & rust →
- 2
Dress welds
Remove the excess, smooth the scratches. Don't dwell in one spot: heat warps thin sheet metal.
Move on when: The weld is flush: running the flat of your hand across it, you can no longer feel a step.
- 3
Key metal
Evenly matt and grease-free – the key for primer and paint.
Move on when: The whole surface is evenly matt, with no glossy spot and no scratch from the coarser grit left.
- 4
Refine the surface
An even scratch pattern for parts that stay bare or get a clear coat.
Move on when: A uniform scratch pattern under raking light, with no stray deeper scratches.
Dashed grits belong to the work step but are not yet in the range for Metal – the link explains what the grit does.
The whole sequence at once
4 grits, 1 × smallest pack each: PRO CUT 150 (10 pcs) P80 · P120 · P180 · P240. We don’t stock P60 for this yet. P60 is available for 125 mm backing pads as PRO CUT 125.
incl. VAT, plus shipping
Matching products
6 products for Metal – recommended ones first, each card starts with the grit you need first here.
Abrasives
- Bestseller
- P80–P600
- Grit
- 150 mm
- Diameter
- 50 pcs
- Contents
€0.50 / pc · incl. VAT, plus shipping
- 152 × 229 mm
- Dimensions
- 10 pcs
- Contents
- very fine (grey)
- Type
€1.49 / pc · incl. VAT, plus shipping
- P80–P400
- Grit
- 70 × 420 mm
- Dimensions
- 25 pcs
- Contents
€0.92 / pc · incl. VAT, plus shipping
Machines
What matters with Metal
What counts beyond the grit – technique, typical defects and the related guides.
Tips from the workshop
01
Rough-grind first, then random orbital
Pre-grind thick welds and mill scale with an angle grinder and flap disc first. The random orbital sander takes over from P60 to P80 – it sands flat and leaves no deep scratches.
02
Avoid heat
Metal conducts heat: thin sheet warps and stainless steel gets heat tint. Sand in passes, don't dwell in one spot, and change the disc as soon as it rubs instead of cutting.
03
Dedicated discs for stainless steel and aluminium
Particles from ordinary steel embed themselves in stainless steel and aluminium and later rust there as flash rust. Use dedicated, labelled discs and non-woven abrasive for these metals.
04
Bare means: prime straight away
Freshly sanded steel develops flash rust within a few hours. Blow off the dust, degrease with silicone remover and prime the same day.
What can go wrong
View all sanding defects →The rust comes back in the same spot
Weeks or months after the repair, the paint bubbles again in exactly the same spot.
Usually: Rust was left in the pores – under a bubble, the rust is almost always bigger than the bubble.
Related guides · 7 articles
Sanding metal: rust, welds, paint prep
Removing rust and mill scale, dressing welds, keying bare metal for primer – which grit for what, and how to tell it is too coarse.
P60 → P120 → P240 → P400
Read · 2 minSanding kerb damage on alloy wheels
Remove the burr with P120, feather the edges with P240, key with P400 before painting: this is how the rim edge gets smooth again – and when a wheel belongs in a specialist workshop.
P120 → P180 → P240 → P320 → P400
Read · 1 minKeying and painting a radiator
Spot-treat rust with P120, matt down the rest with P240 or abrasive fleece – and why you should keep the machine away from the fins.
P120 → P180 → P240
Read · 1 min
FAQ on Metal
Which grit do I use to remove rust?
Heavy rust and mill scale with P40 to P60, flash rust with P80. Then smooth the sanding marks with P120 before primer or paint goes on.
How fine do I sand metal before painting?
For a good key, P120 to P180 is enough – the surface should be evenly matt and grease-free. Finer than P240 gives the primer less grip.
Can I sand stainless steel and aluminium with the same abrasives?
Yes, but with dedicated discs: steel particles on stainless steel or aluminium lead to flash rust later. On aluminium, coarse grits clog quickly – use light pressure and change discs more often.
Which grit do I use to blend a weld?
Take off the excess with P60 to P80 – pre-grind thick welds with an angle grinder first. Then smooth the scratches with P120 and key with P180 to P240 before painting. Don't dwell in one spot: heat warps thin sheet metal.
Disc, sanding roll or non-woven – what do I use for metal?
Flat surfaces with a hook-and-loop disc on the random orbital sander. Tubes, bars and profiles by hand with a sanding roll – the strip wraps around the workpiece. Non-woven abrasive mattes edges, swage lines and curved parts evenly without scratches – ideal right before priming.
More applications
Different surface, different process – each application with its own work steps and grits.
 Car & paintPerfect surfaces – from repair to finishP80 – P3000
 WoodFrom raw to perfect – for furniture, interiors and moreP40 – P320
 PlasticSand safely – for optimum adhesion and perfect resultsP180 – P1000
 Body fillerLevel fast – shape cleanly – prepare perfectlyP80 – P240
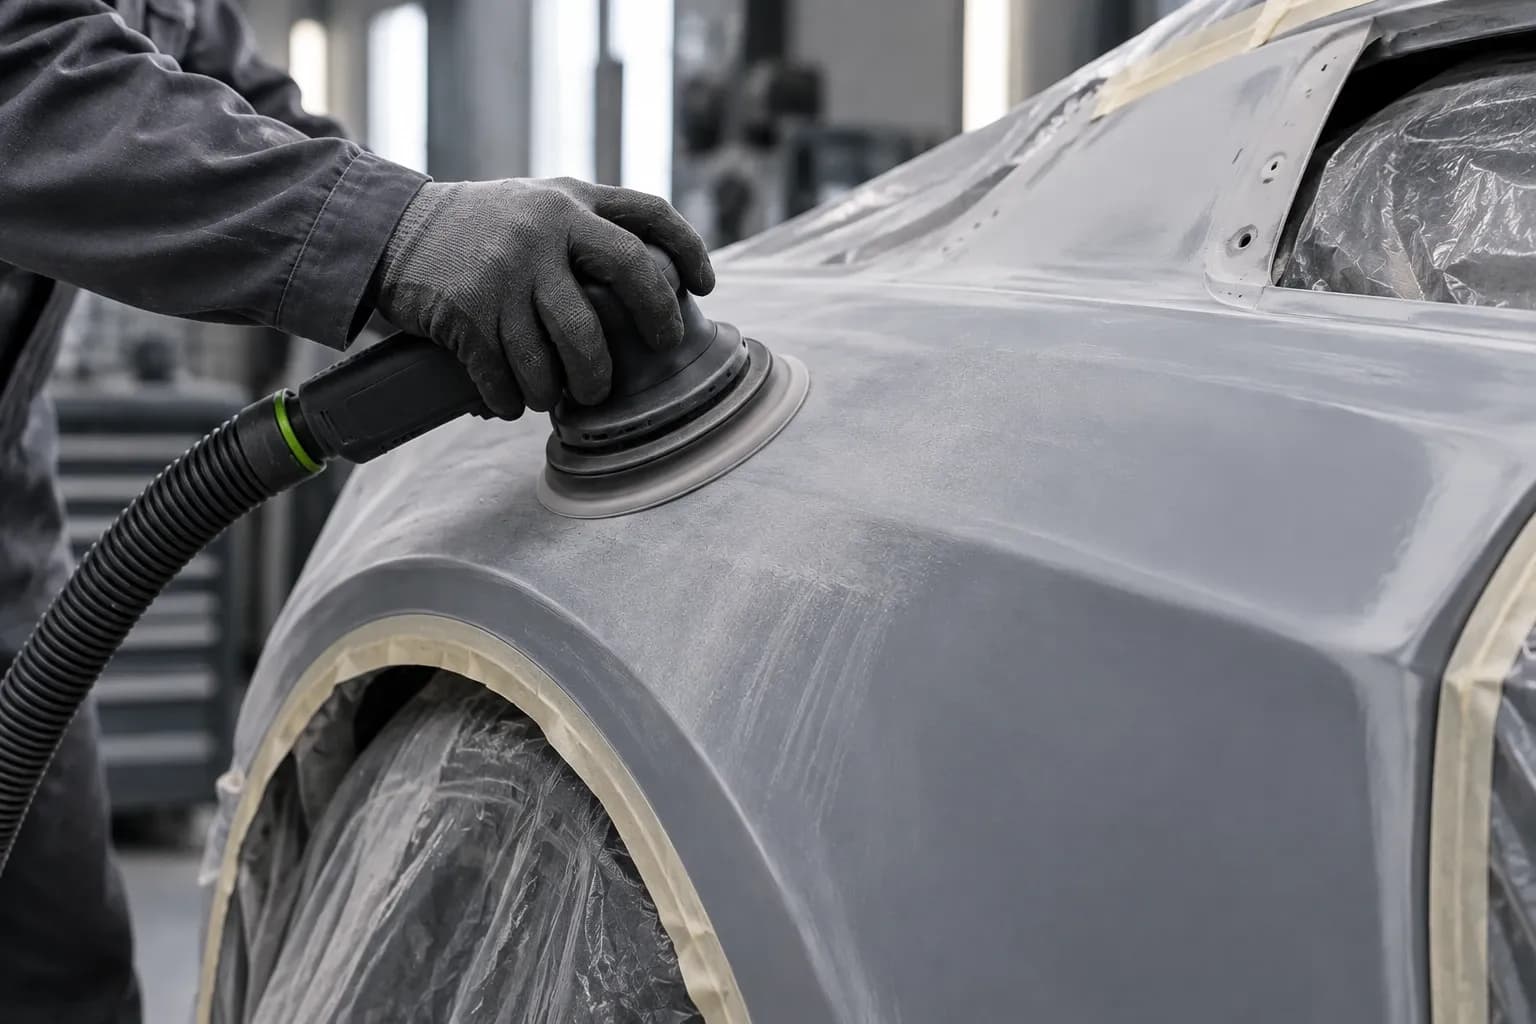 PrimerFor an even, high-quality paint finishP320 – P600
Still unsure?
The abrasive finder asks about your machine and goal – the material is already set – and tells you the product and grit.
Find abrasives for Metal →